White paper 07 · Chapter 6
Wastes and by-products: most residues can become products, but the hazardous dust needs a secure route before start-up
At full capacity, our planning estimates put the main process residues at about 185,000 t a year. About 149,000 t of that would be EAF slag, about 20,000 t mill scale and about 16,000 t EAF dust. Slag and mill scale have established uses as construction aggregate and as recycled iron. EAF dust is different. It is classed as hazardous because it concentrates zinc, lead and cadmium, and we know of no licensed facility in the Océan department that can treat it. The decisive commitment in this chapter is therefore a matter of timing: a compliant route for EAF dust will be secured before the furnace is first lit. That route is either zinc recovery abroad under the Basel and Bamako Conventions, or stabilisation and a permitted secure cell.
In this chapter (6)
6.1 What an EAF works leaves behind
Steelmaking is efficient in its use of materials. worldsteel’s indicators put the industry’s material efficiency, the share of solid materials converted to products and co-products, at 92.8% in 2024, against 97.6% in 2022 [T01]. On average, each tonne of steel made in an EAF yields about 200 kg of co-products, and slags make up about 90% of the industry’s solid co-products by mass [T02]. The IFC EHS Guidelines give a benchmark of 110 to 180 kg of solid waste per tonne of EAF steel [G03]; most of it is slag.
Our planning model applies these benchmarks to the planned capacities. It assumes 140 kg of EAF slag per tonne of liquid steel (within the IFC solid-waste range of 110 to 180), 15 kg of EAF dust (planning range 10 to 20; the European reference document reports 10 to 30 [G17]) and 20 kg of mill scale per tonne of product (range 15 to 25) [X03][G03]. Figure 6.1 shows the result by phase. For comparison, the Malaysian EAF works reviewed by the IFC in 2026 reports about 6,000 t of EAF dust a year from 600,000 t of steelmaking capacity, or about 10 kg per tonne. It reports about 70,000 t of EAF slag (about 117 kg per tonne) and 18,000 t of ladle slag [T08]. Our planning values are deliberately conservative.
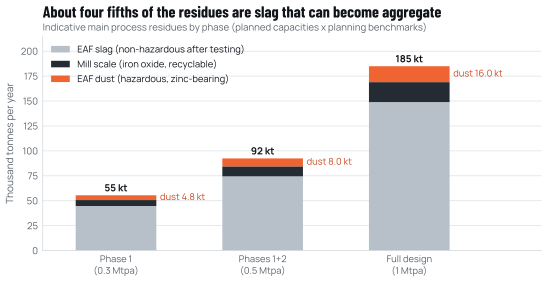
Source: Cameroon Steel planning model, 10 October 2026 [X03]; IFC solid-waste benchmark [G03]; dust planning range [X03][G17]. Indicative values; ladle slag, refractories and minor wastes not shown.
Beyond the three main streams, an EAF long-products works generates several smaller ones:
- ladle-furnace slag;
- spent refractory linings from furnaces and ladles;
- sludges from the water-treatment circuits;
- used oils and greases;
- electrode stubs;
- packaging;
- workshop and office waste;
- during construction, cleared vegetation, spoil and building waste.
Table 6.1 lists each stream with its nature, first-choice outlet and fallback. The assessment will quantify the minor streams once the design is fixed.
Table 6.1 Residue register: nature, first-choice outlet and fallback (planned)
| Residue | Nature | Indicative quantity at full capacity | First-choice outlet | Fallback |
|---|---|---|---|---|
| EAF slag | Non-hazardous after testing; hard, dense, angular | About 149,000 t a year | Road base and asphalt aggregate after ageing, metal recovery and leach testing | Engineered stockpile on site pending market |
| Ladle-furnace slag | Fine, alkaline, may disintegrate to powder | To be quantified | Trials as cement raw material or soil stabiliser | Lined storage on site |
| EAF dust | Hazardous; zinc, lead, cadmium, chlorides | About 16,000 t a year | Zinc recovery in a Waelz kiln, exported under the Basel and Bamako rules | Stabilisation and disposal in a permitted secure cell |
| Mill scale | Iron oxide with traces of oil | About 20,000 t a year | Briquetting and recharge to the EAF, or sale as iron units | Sale to cement producers as an iron corrective |
| Water-treatment sludges | Iron-rich; oily fraction possible | To be quantified | De-oiling and recharge with mill scale | Approved hazardous-waste operator |
| Spent refractories | Mostly inert ceramic | To be quantified | Supplier take-back or reuse as slag conditioner | Inert landfill |
| Used oils and greases | Hazardous | To be quantified | Approved recycler (re-refining) | Approved hazardous-waste operator |
| Construction spoil and cleared vegetation | Inert; timber and biomass | To be quantified | Reuse of spoil on site; timber salvage under the forest law | Approved disposal; no open burning |
Source: IFC EHS Guidelines [G03]; worldsteel co-products [T02]; Décret 2012/2809/PM [L06]; Cameroon Steel planning model [X03]. Quantities indicative and rounded.
6.2 Slag: from residue to aggregate
EAF slag forms when lime and other fluxes combine with the oxides of the metallic charge. Once cooled and crushed it is a hard, dense, angular stone. Around the world it is used as road base, in asphalt wearing courses, as railway ballast and in hydraulic structures. The IFC guidelines note the sale of steel slags for civil engineering, road building and cement making [G03]. worldsteel describes the same uses and notes that, in some uses, physical properties rather than chemistry determine suitability [T02].
Two technical conditions must be met before slag leaves a site as a product. First, the slag must be volume-stable. Steel slags can contain free lime and magnesia, which expand slowly when they react with water. If laid too early they can crack roads. The standard remedy is ageing in weathered stockpiles for several months, with regular wetting and turning, followed by expansion testing. Second, the slag must not leach harmful substances. worldsteel’s position is that leachate criteria for slags in road construction should match those applied to natural aggregates [T02]. We will test every production batch with a recognised leaching test, such as EN 12457, before release (Table 6.2).
The market exists. The road and motorway network around Kribi is expanding. An international tender to reconstruct the 110 km Édéa to Kribi road was signed in February 2025 [K09]. The industrial zone will itself need large volumes of fill and pavement for internal roads and platforms [K02]. A cement plant has operated in the zone since 2024 [K10]. A locally produced aggregate that meets specification can substitute for quarried stone, reducing quarrying elsewhere in the coastal strip.
One regulatory point needs early attention. We found no Cameroonian framework that defines when a processed residue ceases to be waste and becomes a product. Without one, a road contractor buying slag aggregate could be treated as receiving waste. We will ask MINEPDED, as part of scoping, to agree product criteria for processed slag, including stability and leaching limits and traceability by batch. The criteria would be written into the environmental certificate, giving buyers and regulators the same reference.
6.3 EAF dust: the hazardous fraction
EAF dust is the fine material caught by the melt shop’s bag filters. Its composition depends on the charge. Galvanised scrap brings zinc, coated scrap brings lead and cadmium, and plastics and salts bring chlorides. Dust from a charge rich in galvanised scrap carries enough zinc to make it both a hazard and a resource. Cameroonian law treats it as industrial hazardous waste [L06]. Only approved operators may handle it. The generator needs an environmental permit, must keep a register and must track every consignment with a manifest [L06].
Three management routes exist:
- Zinc recovery. In a Waelz kiln, EAF dust is heated with a reducing agent. The zinc volatilises, re-oxidises and is collected as a concentrate for zinc smelters, while the residue can be used in construction [T02]. Waelz kilns need large feed volumes, and none is known to operate in Central Africa. Recovery would therefore mean export. The Basel Convention governs transboundary movements of hazardous wastes. Within Africa, the Bamako Convention bans imports of hazardous wastes into the continent and controls movements between African states [G15]. Export to a recovery facility requires prior informed consent from the importing and transit countries, and documentation from start to finish.
- Recirculation and enrichment. Part of the dust can be injected back into the EAF. This raises the zinc content of the remaining dust and makes recovery more economic. It reduces the volume but does not remove the need for an outlet.
- Stabilisation and secure disposal. Dust can be mixed with binders to immobilise metals, tested for leaching, and placed in an engineered cell with liners, leachate collection and groundwater monitoring. It is the fallback, not the preferred route, because it locks away zinc that could be recovered.
The Malaysian works reviewed by the IFC collects its EAF dust in silos for zinc extraction or reuse [T08]. That is the practice we intend to follow. The decisive point is timing. A melt shop produces dust from its first heat. If no outlet is ready, dust accumulates in temporary storage, and temporary storage of hazardous dust in an equatorial climate is exactly where problems begin.
We will therefore treat a signed contract with a licensed recovery facility, or a permitted secure cell on site, as a condition of starting the furnace. Until dust leaves the site, it will be held in sealed silos or closed bags inside a roofed, bunded store, with a maximum storage period set in the waste management plan. The register and manifests will be open to inspection by MINEPDED and to the independent monitor described in Chapter 10.
6.4 Mill scale, sludges, refractories and the rest
Mill scale is the iron oxide that forms on hot steel and flakes off during casting and rolling. It is collected in the scale pits of the direct-contact water circuits. It is one of the most valuable residues of a steelworks, a rich source of iron units. Once de-oiled, it can be briquetted with a binder and recharged to the EAF, or sold to cement producers who use iron oxide to correct their raw-material chemistry. Water-treatment sludges can follow the same route after de-oiling.
Spent refractories are mostly inert ceramic. Suppliers increasingly take them back for recycling, and some magnesia-based materials can replace part of the lime used to condition slag. Used oils will go to an approved recycler. Electrode stubs are reused in the furnace. General waste will be segregated at source, with recyclables separated. Nothing will be burned in the open, on site or by contractors.
6.5 The register, the tests and the zone
Good residue management is mostly a matter of records and discipline. Our waste management plan will rest on four elements:
- a register that tracks every stream from generation to final outlet;
- segregated, labelled and roofed storage, with bunding for liquids and hazardous materials;
- testing before any residue leaves as a product (Table 6.2);
- audits of every contractor and receiving facility before first use and at least once a year thereafter.
Table 6.2 Tests before a residue leaves the site as a product (planned)
| Residue | Test | Frequency | Release criterion |
|---|---|---|---|
| Processed EAF slag | Leaching (EN 12457 or equivalent); volume stability (expansion test); grading and strength | Each production batch, plus quarterly full characterisation | Leachate within criteria for natural aggregates agreed with MINEPDED; expansion within road-specification limits |
| Mill scale and de-oiled sludge | Oil content; iron content | Each consignment | Oil content below the receiving process’s specification |
| EAF dust (for export) | Zinc, lead, cadmium, chlorides, moisture | Each consignment | Within the receiving facility’s acceptance criteria; manifest complete |
| Stabilised dust (if disposed) | Leaching after stabilisation | Each batch | Within the secure cell’s permitted criteria |
| Secure cell and stockpiles | Groundwater wells up- and down-gradient | Quarterly | No statistically significant increase over baseline |
Source: IFC EHS Guidelines [G03]; worldsteel co-products [T02]; Décret 2012/2809/PM [L06]; Cameroon Steel objectives (planned).
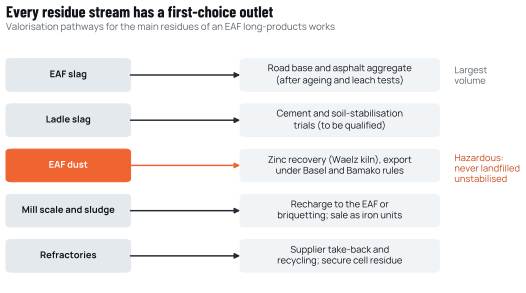
Source: IFC EHS Guidelines [G03]; worldsteel [T02]; Décret 2012/2809/PM [L06]; Basel and Bamako Conventions [G15].
A wider problem lies beyond any single tenant. We found no information on a shared hazardous-waste facility, engineered landfill or slag processing area planned for the industrial zone. As heavy industry arrives in Kribi, each tenant building its own small secure cell would be costly and hard to supervise. We will propose to the zone’s management that the tenants and the authorities jointly assess shared facilities, from slag processing and a licensed hazardous-waste transfer station to an engineered landfill. We will contribute our data and a share of the study’s cost.
6.6 Construction waste and cleared vegetation
The construction phase brings its own residues: vegetation from clearing, topsoil, excavated spoil, concrete and steel offcuts, packaging and workers’ camp waste. Clearing will follow the forest law, including the salvage and declaration of any merchantable timber [L15]. Topsoil will be stripped and stockpiled for later landscaping and for the green belt. Spoil will be balanced across the site wherever the earthworks design allows, to limit haulage. Contractors will be bound by a construction waste plan with the same register, segregation and no-burning rules as the operating plant. Compliance will be checked by the site environmental team and reported in the half-yearly reports to MINEPDED.
A residue register from the first day of construction. Slag released as aggregate only after ageing and batch leach testing, against product criteria agreed with MINEPDED. A contracted, compliant outlet for EAF dust before the first heat. No open burning. A proposal to the zone for shared slag and hazardous-waste facilities. Annual publication of residue quantities and the share recovered.
Sources cited in this chapter
Bracketed markers refer to these sources; the full list is in the annex. Full list of sources
- T01Sustainability Indicators Report 2025 (2024 data). World Steel Association (worldsteel), Nov 2025 (updated Feb 2026).worldsteel.org/wider-sustainability/sustainability-indicators/
- T02Steel industry co-products. World Steel Association (worldsteel).worldsteel.org/wider-sustainability/steel-industry-co-products/
- G03Environmental, Health, and Safety Guidelines for Integrated Steel Mills. IFC / World Bank Group, 30 Apr 2007.ifc.org/content/dam/ifc/doc/2000/2007-integrated-steel-mills-ehs-guide…
- G17Best Available Techniques Reference Document for Iron and Steel Production (EUR 25521). European Commission, Joint Research Centre, 2013.bureau-industrial-transformation.jrc.ec.europa.eu/sites/default/files/…
- X03Cameroon Steel reference configuration RC-1 (planning estimate): planned capacities, phases, indicative schedule and benchmark-based estimates, edition of 10 October 2026. Cameroon Steel, 10 Oct 2026.Cited by title and date
- T08Environmental and Social Review Summary 51259, Esteel Loan (EAF steel and rebar works, Malaysia). International Finance Corporation, 6 Jan 2026.disclosures.ifc.org/project-detail/ESRS/51259/esteel-loan
- L06Décret n° 2012/2809/PM fixant les conditions de tri, collecte, stockage, transport, récupération, recyclage, traitement et élimination finale des déchets; Arrêtés n° 001 and 002/MINEPDED. Prime Minister; MINEPDED, 26 Sep 2012; 15 Oct 2012.faolex.fao.org/docs/pdf/cmr195749.pdf
- K09Bilan et perspectives: les voyants sont au vert. Port Autonome de Kribi, 13 Mar 2025.Cited by title and date
- K02Zone industrialo-portuaire de Kribi (KPIZ): jusqu’à +8 points de croissance et 150 000 emplois attendus sur 15 ans. Investir au Cameroun, 4 Mar 2026.investiraucameroun.com/gestion-publique/0403-23163-zone-industrialo-po…
- K10La zone industrialo-portuaire de Kribi rayonne avec l’inauguration de la cimenterie CIMPOR. Port Autonome de Kribi, 19 Jul 2024.Cited by title and date
- G15Basel Convention on the Control of Transboundary Movements of Hazardous Wastes and their Disposal; Bamako Convention on the Ban of the Import into Africa and the Control of Transboundary Movement and Management of Hazardous Wastes within Africa. Secretariat of the Basel Convention (UNEP); African Union, 22 Mar 1989; 30 Jan 1991.basel.int
- L15Loi n° 2024/008 portant régime des forêts et de la faune. Presidency of the Republic, 24 Jul 2024.prc.cm/fr/actualites/actes/lois/7298-loi-n-2024-008-du-24-juillet-2024…
Cite this chapter
Cameroon Steel (2026). Building responsibly in Kribi: a steelworks can meet international standards on four conditions. White paper 07, chapter 6: Wastes and by-products: most residues can become products, but the hazardous dust needs a secure route before start-up. CS-WP-07. https://www.cameroon-steel.com/en/library/responsible-kribi/wastes-by-products/
Source