White paper 03 · Chapter 8
Digitalisation and automation: control systems are part of the process, not an add-on
A modern melt shop and mill cannot reach their design yield, energy use and quality without automation, and a new plant has the advantage of designing it in from the start. Basic automation (Level 1) and process models (Level 2) control the furnace, the ladle, the caster and the mill second by second; a manufacturing execution system (Level 3) links every bundle to the heat it came from; and an energy-management system turns metering into savings. Manufacturing plants certified to ISO 50001 improved their energy performance by about 4.1% in the first year and still by about 3.4% a year twelve years later [S31]. For Phase 1’s planned electricity use of about 289 GWh a year (about 302 GWh at the upper electricity value), a 4% improvement would be worth about 12 GWh a year (derived) [S03]. The same data thread is what customers, regulators and, for exports to Europe, carbon border rules increasingly require.
In this chapter (13)
- 8.1 Five levels of control, each with its own clock
- 8.2 Levels 1 and 2 in the melt shop: models that save minutes and kilowatt-hours
- 8.3 Level 2 in the mill: pass schedules, quench control and measurement
- 8.4 Energy management turns metering into savings
- 8.5 Traceability: every bundle back to its heat
- 8.6 Carbon accounting from the first heat
- 8.7 Simulation before construction, and for training
- 8.8 Phasing the digital investment
- 8.9 Reliability: maintenance driven by data
- 8.10 Cybersecurity and architecture
- 8.11 People make the systems work
- 8.12 Records that outlive the plant’s first owners
- 8.13 What digitalisation means for the decision
8.1 Five levels of control, each with its own clock
Industrial automation is usually described with the functional hierarchy of the ISA-95 standard (IEC 62264), shown in Figure 8.1. Level 0 is the physical process with its sensors and actuators. Level 1 is basic control in programmable logic controllers and distributed control systems, responding in fractions of a second. Level 2 is supervisory control and process optimisation. Level 3, manufacturing operations management, works on time frames of days, shifts, hours and minutes and covers scheduling, quality, maintenance and inventory. Level 4, enterprise planning and logistics, works in months, weeks and days through enterprise resource planning [S101].
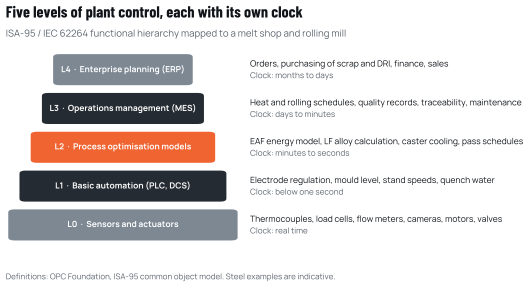
Source: Cameroon Steel; level definitions from the OPC Foundation’s ISA-95 common object model [S101].
The value of the hierarchy is practical: it tells the plant’s designers which system owns which decision and how data must flow between them. A recurring failure in steel plants is a gap between levels, for example a caster that records billet data that never reach the mill, or a laboratory whose test results are typed by hand into a certificate.
8.2 Levels 1 and 2 in the melt shop: models that save minutes and kilowatt-hours
In an electric arc furnace, Level 1 regulates the electrodes continuously to keep the arcs stable, controls the oxygen and carbon injectors and burners and protects the water-cooled panels. Level 2 adds models: an energy and mass balance that estimates the bath’s temperature and chemistry between measurements, a power programme that chooses transformer taps through the heat, and, in the ladle furnace, an alloy calculation that finds the cheapest additions to reach the target chemistry. In the caster, Level 1 controls mould level and strand speed, while Level 2 calculates secondary cooling to avoid cracks.
Several suppliers offer these functions as packages. Tenova, for example, describes its iEAF system as a modular package built on full off-gas analysis, sensors, process models and advanced control, claiming savings in electricity, fuel, power-on time, tap-to-tap time, yield, electrodes and refractories [S102]. Claims of this kind vary widely between plants; the right approach for a new plant is to specify the measurements and models in the furnace contract and to agree performance tests.
For the Phase 1 furnace, where a single EAF must run about 7,300 to 7,900 hours a year to reach nameplate (Chapter 5), every minute of power-on time saved is capacity gained. A model that helps the operator tap at the right temperature, avoid over-heating and charge the right mix of scrap and DRI is worth more in a single-furnace shop than in a large multi-furnace plant.
8.3 Level 2 in the mill: pass schedules, quench control and measurement
In the rolling mill, Level 2 stores a pass schedule for every product, sets roll gaps and speeds, controls the tension between stands and runs the quench water for rebar according to bar size and target properties. Laser gauges after the finishing stands measure every bar’s dimensions; pyrometers measure temperature before and after the quench. For wire rod, the controlled-cooling conveyor runs a recipe for each grade. These systems make product changes fast and repeatable, which is what allows a mill to serve a market of many diameters without long stops.
8.4 Energy management turns metering into savings
Energy is the largest variable cost of an electric steelworks after iron units, and it is also the largest source of its emissions. An energy-management system meters electricity by unit (furnace, ladle furnace, caster, heater, mill, utilities), links consumption to production and identifies deviations. Certification to ISO 50001 formalises the process. A study of 83 certified manufacturing facilities found average energy performance improvements of about 4.1% in the first year and about 3.4% a year twelve years after implementation [S31].
RC-1 estimates Phase 1 electricity use at about 289 GWh a year and an average load of about 36 MW at the planning value of 450 kWh per tonne in the furnace, or about 302 GWh and 38 MW at the upper value of 490 kWh [S03]. On that basis, a 4% improvement would save about 12 GWh a year (derived). The same system serves the power-system relationship described in Chapter 5: it can schedule furnace power-on periods around the grid’s peaks and within the plant’s contracted capacity on the 225 kV line, coordinate with the compensator and report power quality at the connection point.
8.5 Traceability: every bundle back to its heat
Traceability is where automation meets the customer. Figure 8.2 shows the chain of identifiers that a long-products plant maintains: the charge lot of scrap and DRI, the heat number with its chemistry and temperatures, the billet with its strand and casting data, the rolling lot with its pass and quench settings, the tag on each bundle or coil, and the mill certificate, usually a type 3.1 inspection certificate under EN 10204, that accompanies the delivery.
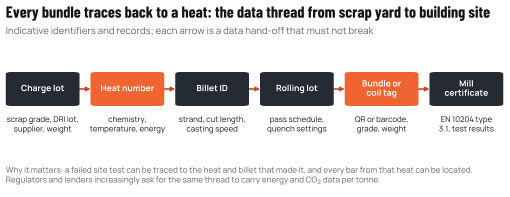
Source: Cameroon Steel.
In Cameroon, where the standards agency has withdrawn a compliance certificate and ordered the recall of non-compliant rebar [S26, S27], traceability protects the honest producer: a failed site test can be traced to its heat, the other bars from that heat located and tested, and the cause found. It also supports certification by ANOR and by export certification schemes.
The same thread will carry carbon data. The EU Carbon Border Adjustment Mechanism, in its definitive phase since 1 January 2026, requires importers of iron and steel products to declare the emissions embedded in them [S53]. Producers that can report verified, installation-specific emissions per tonne avoid being assessed on default values, and the importer’s charge depends on those emissions. Measuring CO2 per heat and per product from the first day of operation is therefore a commercial asset for any export to Europe, and a requirement that lenders are likely to set in any case.
Table 8.1 Digital systems for the Kribi steelworks, by level and value
| Level | System | Main functions | Value for the plant | Phase |
|---|---|---|---|---|
| 0 and 1 | Sensors, electrode regulation, PLC and DCS | Stable arcs, mould level, stand speed, quench water, safety interlocks | Safe, stable operation; the basis of every other level | Phase 1, built in |
| 2 | EAF and ladle-furnace process models | Energy and mass balance, power programme, alloy calculation | Shorter power-on time, fewer re-blows, lower alloy cost | Phase 1 |
| 2 | Caster and mill models | Secondary cooling, pass schedules, quench recipes, laser gauging | Yield, dimensional quality, repeatable product changes | Phase 1 |
| 2 and 3 | Power-quality and energy management (ISO 50001) | Metering by unit, demand control, flicker and harmonics monitoring | About 4% energy improvement in the first year in certified plants [S31]; grid compliance | Phase 1 |
| 3 | Manufacturing execution system and laboratory system | Heat and rolling schedules, traceability, certificates, maintenance | Certified product, recall capability, reliability | Phase 1 |
| 3 | Emissions monitoring, reporting and verification | CO2 per heat and product, carbon footprint | CBAM declarations based on actual data [S53]; lender reporting | Phase 1, extended with DRI |
| 4 | Enterprise resource planning | Orders, metallics purchasing, finance, logistics | Working capital, supply security | Phase 1 |
Source: Cameroon Steel; functions per ISA-95 levels [S101].
8.6 Carbon accounting from the first heat
Measuring CO2 is an engineering task before it is a reporting task. The international method for calculating the CO2 intensity of steel production, ISO 14404, counts the carbon in every input (electrodes, charge carbon, natural gas, purchased DRI and electricity) and in every output (steel, slag, dust), and allocates emissions across the plant’s boundary. A plant that meters each input, weighs each output and links both to heats and rolling lots can produce a footprint for each product, rather than a site average.
That capability matters for three audiences. EU importers must declare the emissions embedded in iron and steel products under the CBAM regulation, and actual, verified data are preferable to default values [S53]. Development lenders increasingly require project-level greenhouse-gas reporting. And domestic buyers, notably public works and international contractors, are beginning to ask for product carbon footprints. RC-1’s estimated intensities, about 0.32 t CO2 per tonne of finished product for scope 1 and 2 in Phase 1 and about 0.33 t at full build-out [S03], will be replaced by measured values once the plant runs.
8.7 Simulation before construction, and for training
Two kinds of model reduce risk before the plant is built. The first is an electrical model of the grid connection, the furnace and its compensator, used for the flicker and harmonics study that Gate 1 requires (Chapter 10). The second is a set of process simulators for the furnace, the caster and the mill, which suppliers use to train operators before hot commissioning. Operators who have practised power programmes, breakouts and cobbles on a simulator make fewer costly mistakes on live equipment.
8.8 Phasing the digital investment
Not every system needs to be complete on the first day. The Phase 1 core is non-negotiable: Level 1 control and safety systems, Level 2 models for the furnace, ladle furnace, caster and mill, the laboratory information system, traceability from charge lot to certificate, and energy and emissions metering. Advanced analytics, predictive maintenance models and plant-wide optimisation can follow once the plant has a year of reliable data. What must be right from the start is the architecture: consistent identifiers, a single data model and network segregation, so that later systems can be added without rebuilding the foundations.
8.9 Reliability: maintenance driven by data
A single-furnace melt shop with high utilisation is vulnerable to unplanned stops. Condition monitoring of the furnace transformer, the water-cooled panels and roof, the hydraulic systems and the mill drives allows maintenance to be scheduled before failure. A computerised maintenance system, linked to Level 3, records every intervention and every spare part. The same principle applies to the compensator and the high-voltage substation, whose failure would stop the whole plant.
8.10 Cybersecurity and architecture
Connecting control systems to business systems and to suppliers’ remote-support platforms creates exposure to cyber attack. The ISA-95 hierarchy provides a natural architecture for defence: separate networks for control (Levels 0 to 2) and business (Levels 3 and 4), controlled interfaces between them, and remote access only through monitored gateways. The IEC 62443 series of standards for industrial automation security should be part of the automation specification from the start, because retrofitting security to a running plant is costly.
8.11 People make the systems work
Automation does not reduce the need for skilled people; it changes their skills. A plant of this kind needs automation engineers, instrument and electrical technicians, process engineers who understand both metallurgy and models, and data specialists. Cameroon has a base to build on: the National Advanced School of Engineering in Yaoundé teaches industrial and mechanical engineering, electrical engineering and civil engineering, but has no dedicated metallurgy department [S39], and the University Institute of Technology in Douala trains technicians in mechanical and production engineering, industrial maintenance, thermal engineering and electrical engineering [S103]. Vendor training, simulator-based training for furnace and mill operators, and partnerships with these institutions should be part of the technology contract.
8.12 Records that outlive the plant’s first owners
The records of a rebar plant are needed for as long as the buildings that contain its bars stand. A structural engineer assessing a damaged building, or an investigator after a collapse, may need to know what a bar’s chemistry and tensile results were decades after it was rolled. The plant’s data policy should therefore define what is kept (heat chemistry, test results, certificates, quench parameters), for how long, in what format and with what back-up, and who may access it. The same policy should govern the process data that technology suppliers collect through remote-support connections: Cameroon Steel should own its operating data, decide what leaves the plant, and require suppliers to protect it.
8.13 What digitalisation means for the decision
Digital systems are a small part of the capital cost of a steelworks but a large part of its performance. The decision-maker’s checklist is short: Level 1 and Level 2 functions and their performance tests written into the furnace, caster and mill contracts; a single plant-wide identifier scheme from charge lot to certificate; metering sufficient for ISO 50001 and for product carbon footprints; and an automation architecture designed for security. All of them are cheaper to specify at the start of Phase 1 than to add later.
Sources cited in this chapter
Bracketed markers refer to these sources; the full list is in the annex. Full list of sources
- S101OPC UA Common Object Model: ISA-95 concept. OPC Foundation, Undated, accessed Oct 2026.reference.opcfoundation.org/specs/OPC-10030/4
- S102Intelligent EAF (iEAF) technology. Tenova, Undated, accessed Oct 2026.tenova.com/technologies/intelligent-eaf-ieafr-technology
- S31Fitzgerald P., Therkelsen P. L., Sheaffer P., Rao P., Deeper and persistent energy savings and carbon dioxide reductions achieved through ISO 50001 in the manufacturing sector, Sustainable Energy Technologies and Assessments. Lawrence Berkeley National Laboratory, 2023.eta-publications.lbl.gov/publications/deeper-and-persistent-energy-sav…
- S03Cameroon Steel reference configuration RC-1 (planning estimate): phases, benchmarks with ranges and indicative balances for the Kribi steelworks (Class 5), edition 10 October 2026, values as revised on that date. Cameroon Steel, 10 Oct 2026.Cited by title and date
- S26Cameroon rejects fresh push to revise rebar standard. Business in Cameroon, 26 Jan 2026.businessincameroon.com/construction/2601-15657-cameroon-rejects-fresh-…
- S27Cameroun: le gouvernement rejette une demande de révision de la norme du fer à béton. EcoMatin, 5 Feb 2026.ecomatin.net/cameroun-le-gouvernement-rejette-une-demande-de-revision-…
- S53Regulation (EU) 2023/956 establishing a carbon border adjustment mechanism, Annex I. EUR-Lex, Official Journal L 130, 16 May 2023.eur-lex.europa.eu/legal-content/EN/TXT/PDF/?uri=CELEX:32023R0956
- S39École Nationale Supérieure Polytechnique de Yaoundé: departments. ENSP Yaoundé, Undated, accessed Oct 2026.polytechnique.cm/
- S103Institut Universitaire de Technologie de Douala: departments. IUT Douala, Undated, accessed Oct 2026.iut-dla.cm/
Cite this chapter
Cameroon Steel (2026). Electric steelmaking is the right route for Central Africa. White paper 03, chapter 8: Digitalisation and automation: control systems are part of the process, not an add-on. CS-WP-03. https://www.cameroon-steel.com/en/library/technology-routes/digitalisation/
Source